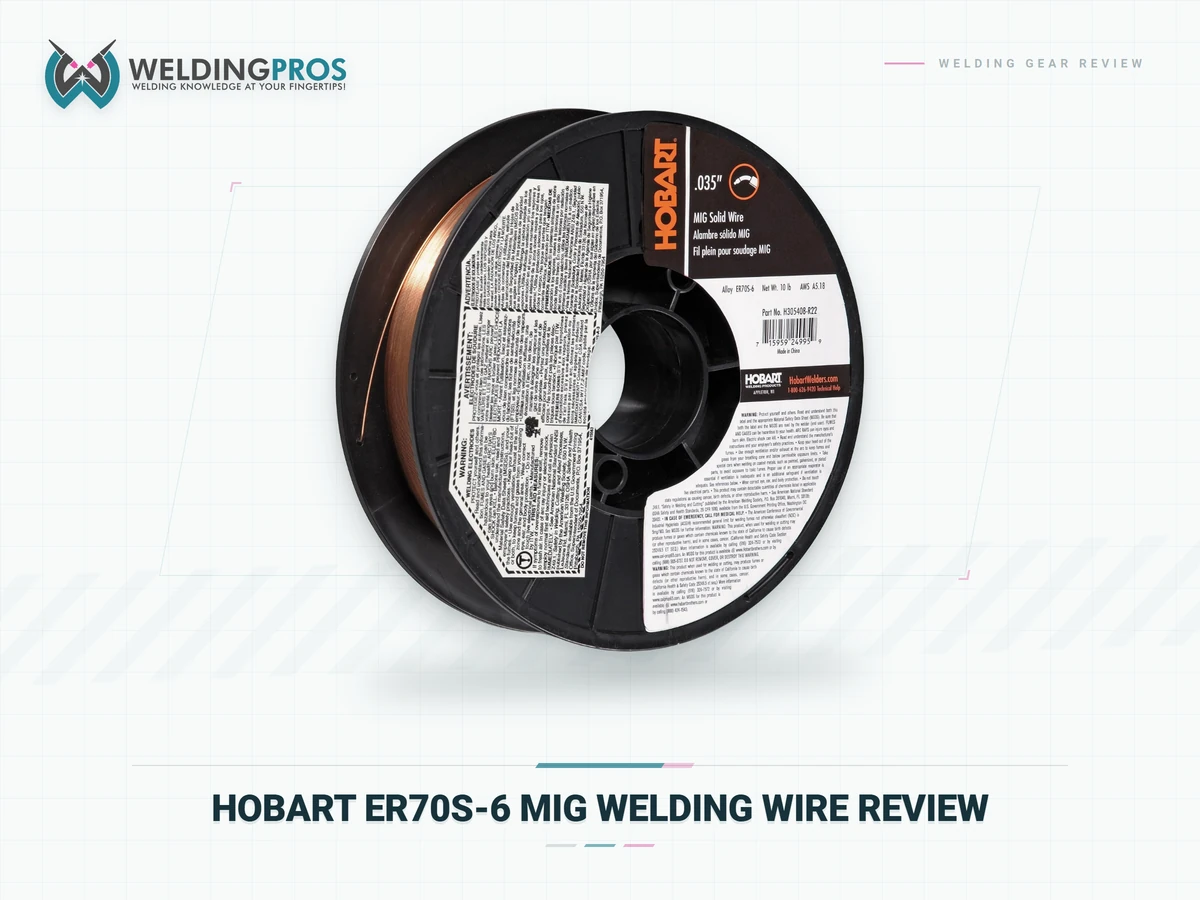
Cheap MIG wire is a false economy, and brand-name wire at box-store pricing is rare enough that I check it twice. That is the pitch behind the Hobart ER70S-6 .035 in. spool, and this Hobart ER70S-6 review checks whether the pitch holds.
We already run this wire on our best MIG welding wire shortlist as the affordable brand-name pick, and it earned that spot honestly. It welds well above its price, with one real weakness I will get to. ER70S-6 is a classification, not marketing.
The 6 suffix means the wire carries extra manganese and silicon deoxidizers compared with an ER70S-3, so it tolerates light rust, mill scale, and oily plate that would turn a lesser wire porous.
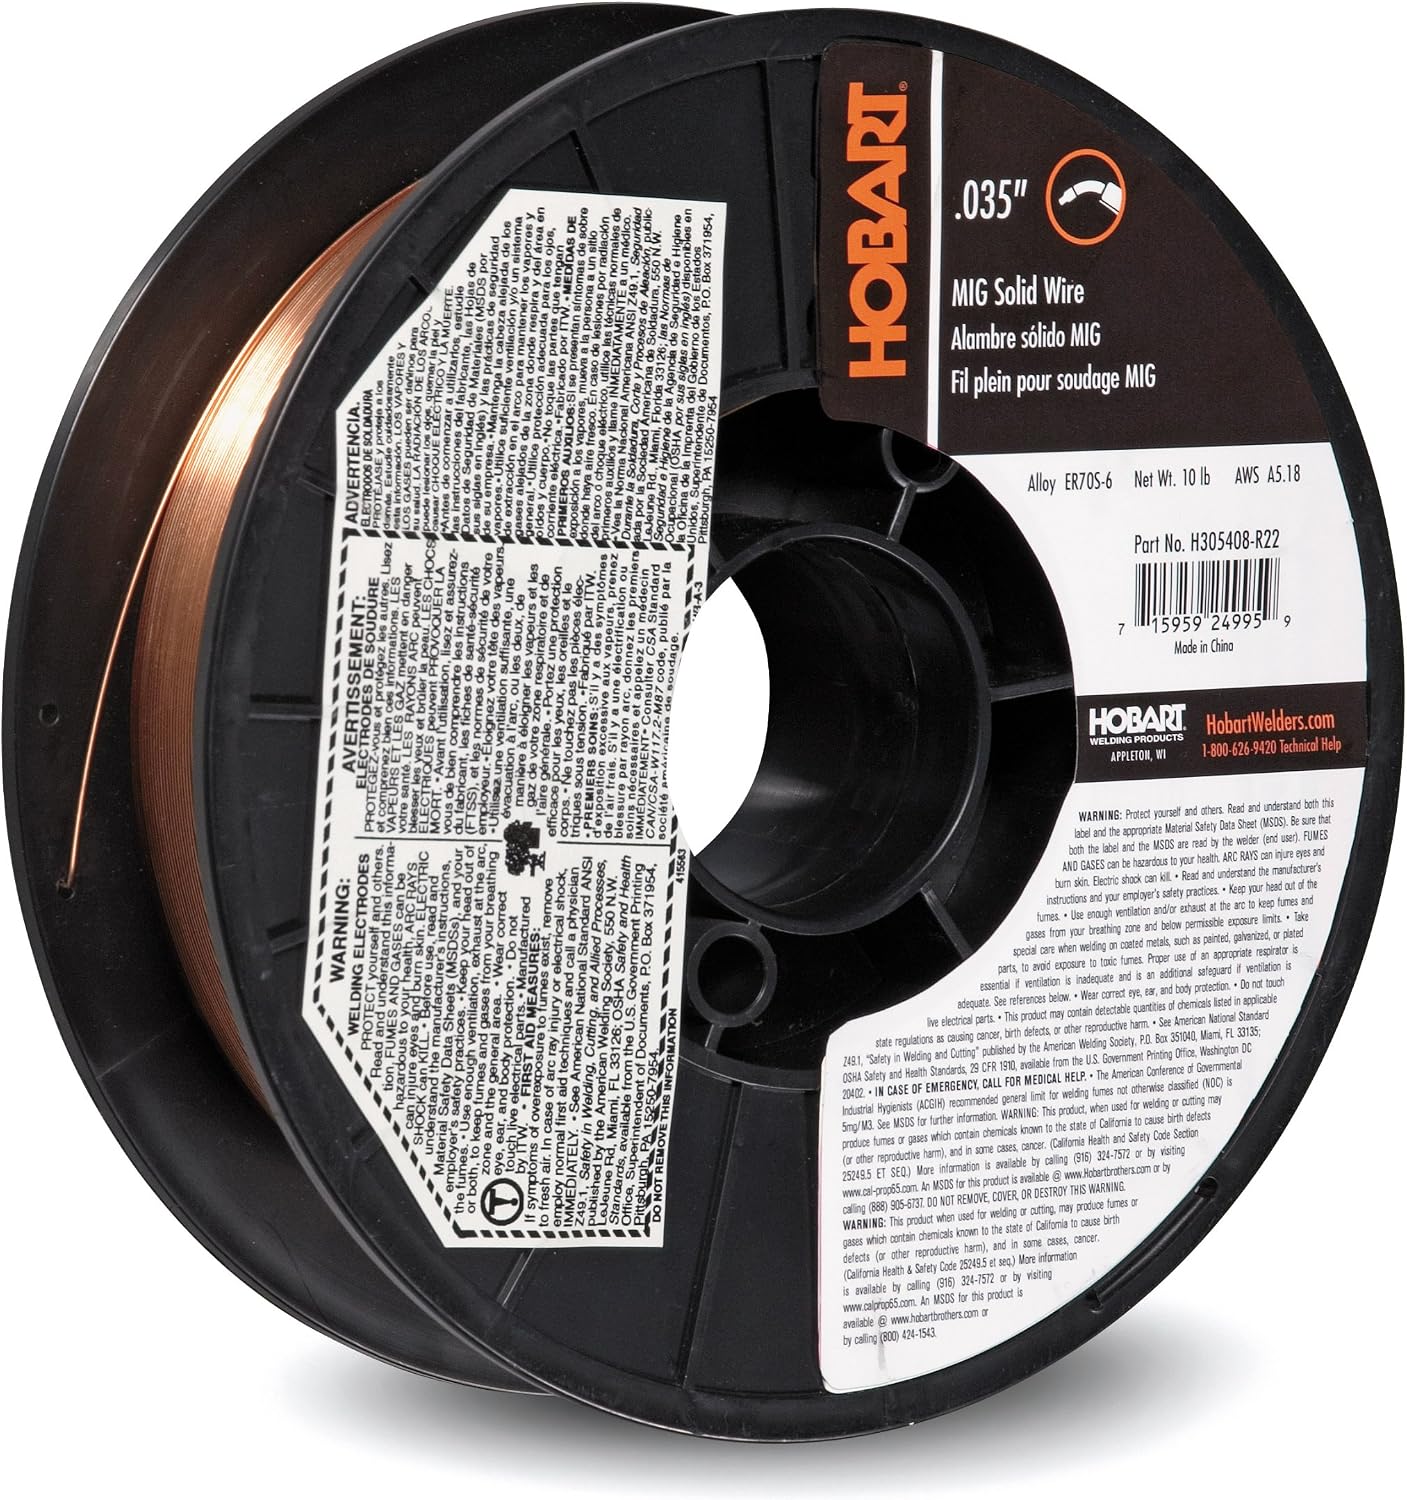
Hobart sells it as the HB-28 line, copper coated, and the spool reviewed here is part number H305408-R22: 10 lb of .035 in. wire on an 8 in. spool. This is a solid wire, which means shielding gas is mandatory. If you need gasless, that is flux core wire and a different review. What the Hobart asks for is a bottle: 75/25 argon CO2 for short circuit work, straight CO2 if you want penetration on a budget, or a 90/10 mix once your machine can push .035 into spray transfer.
The review pulls together Hobart’s published classification data, the AWS A5.18 requirements the wire is built to, what verified owners report after burning spools of it, and what we recorded in our own testing. Where a claim exists only in marketing copy, it stayed out.
Hobart ER70S-6 .035 Carbon Steel MIG Wire Package Content & Technical Specifications
The Hobart arrives as a single 10 lb spool, about 4.5 kg, wound on a standard 8 in. spool with a 2 in. arbor hole that fits every common MIG machine from hobby 140 A boxes upward. There is nothing else in the box, which is normal for wire. Here is what the package gives you:
Brand-Name Wire At A Budget Price
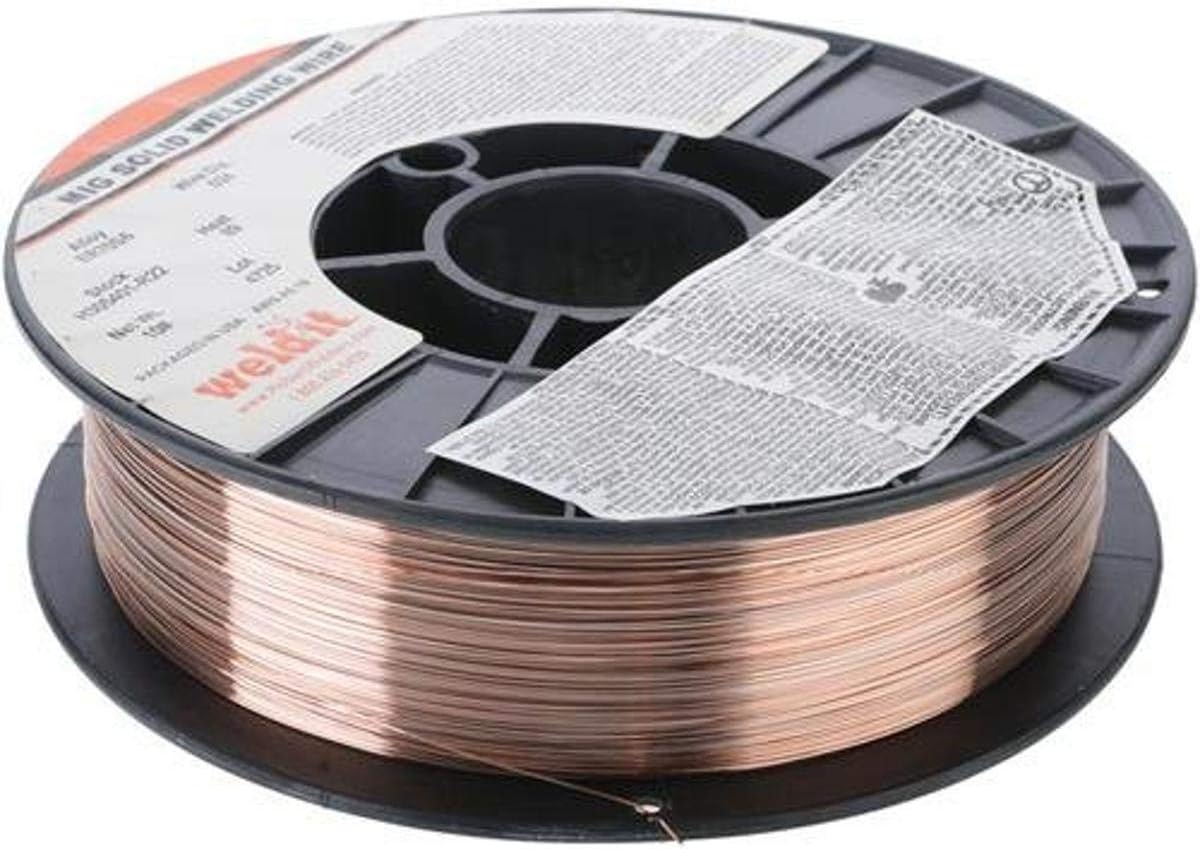
- One 10 lb spool of Hobart ER70S-6 solid carbon steel wire, .035 in. diameter
- Copper coating for conductivity and corrosion resistance
- Standard 8 in. spool with 2 in. arbor hole
- AWS A5.18 ER70S-6 classification and part number H305408-R22 printed on the packaging
- No gas, contact tips, or drive rolls included; the same line is sold in .024 and .030, and as 2 lb spools
- Ships in the Hobart retail carton; inspect it on arrival, since the thin packaging is this wire’s known weak point
- Storage note: keep the spool sealed and dry until use, because even copper-coated wire picks up moisture
Technical Specifications
| Wire classification: | AWS A5.18 ER70S-6 (also ASME SFA 5.18) |
| Trade name / part number: | Hobart HB-28, H305408-R22 |
| Process: | Gas-shielded solid MIG wire (GMAW) |
| Diameter reviewed: | .035 in. (0.9 mm) |
| Line diameters: | .024, .030, .035 in. |
| Spool size: | 10 lb (2 lb also sold), 8 in. spool, 2 in. arbor |
| Shielding gas: | 75/25 Ar/CO2, 100% CO2, or 90/10 Ar/CO2 (spray) |
| Polarity: | DCEP (electrode positive) |
| Tensile strength: | 70,000 psi minimum |
| Yield strength: | 58,000 psi |
| Elongation: | 22% in 2 in. |
| Base metal: | Mild and carbon steel |
| Passes / positions: | Single and multi-pass, all positions |
| Wire finish: | Copper coated |
| Country of origin: | Wound in China for Hobart (Troy, Ohio) |
Pros
- Brand-name consistency and quality control at a budget price
- High deoxidizer load handles light rust, mill scale, and oily plate
- Flat, well-wet beads with low spatter on 75/25
- Full AWS A5.18 and ASME classification data published
- 10 lb spool cuts the per-pound cost for anyone welding weekly
Cons
- Cheap packaging; cartons arrive damaged more often than premium brands
- Needs a shielding gas bottle setup, unlike flux core
- Wound in China for the US brand
- No advantage on thin sheet; .030 or .024 fits that work better
- No machine-specific settings chart in the box; expect a test run on scrap to dial it in
Hobart ER70S-6 Performance
Specifications tell you what a wire promises. The interesting part is how it behaves on real steel, so that is where I spent my time.
The short version: this Hobart runs like wire that costs more. Owners describe a stable arc, flat beads that wet out properly, and porosity-free welds on steel that is less than perfectly clean, which is exactly what the extra deoxidizers are for. Retailer listings for the family sit near 4.8 stars across dozens of reviews, and the .035 spool buys the same chemistry with faster deposition.
Bead Quality, Spatter, and Dirty Steel
The deoxidizer load is the whole story with any S-6 wire, and Hobart does not skimp on it. In practice the wire wets out flat instead of crowning, ties in at the toes evenly, and keeps porosity off plate carrying light mill scale or a flash of surface rust. On clean steel you can push travel speed harder than an S-3 wire would tolerate before the bead starts to rope. Our parent testing and owner reports agree on this: smooth beads, stable arc, low spatter on a 75/25 mix.
It is not magic. Heavily scaled or painted steel still needs grinding back to bright metal, and no deoxidizer package saves a weld laid over an oily puddle. But between clean plate and junk steel sits a wide band of ordinary dirty work, and that band is where the S-6 chemistry pays. Hobart’s own application list for the HB-28 reads the same way: auto body, collision repair, pressure vessels, pipe, steel castings, and thin sheet.
Feeding, Polarity, and Gas Choice
Setup is conventional solid-wire MIG, which came as a relief after a month of flux core. Polarity is DCEP, electrode positive, the factory default on every MIG machine sold today. For .035 you want .035 V-groove drive rolls and a matching contact tip, with tension set just past the slip point. If the feed stutters, fix tension and liner before blaming the spool. Our how to MIG weld guide walks through the full sequence for anyone new to the process.
Gas choice moves the bead more than any dial on the machine. On 75/25 the Hobart runs its quietest arc with the least spatter, which is why that mix is the default for this wire. Straight CO2 costs less per cylinder and digs deeper, at the price of a noisier arc, more spatter, and faster tip wear. A 90/10 argon mix will carry .035 into true spray transfer if your machine has the amperage. Our types of welding gases article lays out the trade-offs in detail.
Strength Numbers and Where I Would Run It
The classification puts minimum tensile strength at 70,000 psi, yield at 58,000 psi, and elongation at 22% in 2 in., and Hobart’s HB-28 data meets those numbers with room to spare. Those are AWS A5.18 class values, the standard governing the ER70S-6 designation, and the wire also carries ASME SFA 5.18 listing for coded work. Single pass or multi-pass, all positions: it is rated for both, which separates it from the single-pass gasless spools sitting next to it on the shelf.
The one honest weakness is the packaging. We flagged it during our parent testing and owners repeat it: the spool wrap and carton are cheap, and a crushed carton can mean a winding that picked up moisture or picked up nicks before you ever opened it.
Order from a retailer that boxes it properly, and store the spool in a dry cabinet or a sealed bag with desiccant once opened. The wire itself is wound overseas for the Ohio brand, which is how the price stays where it is.
Frequently Asked Questions [F.A.Q]
Can I use Hobart ER70S-6 without shielding gas?
No. ER70S-6 is a solid wire and needs gas: 75/25 argon CO2, 100% CO2, or a 90/10 argon mix. Gasless welding calls for flux core wire such as E71T-GS, which is a different product with different polarity.
Is .035 the right diameter for my welder?
.035 suits steel 3/16 in. and thicker and machines from about 140 A upward. .030 is the better pick for sheet metal and auto body work on 120 V machines, and .024 exists for thin stock. The chemistry is identical across diameters, so match the wire to the machine and metal, not the other way around.
What does ER70S-6 mean?
E is electrode, 70 sets the 70,000 psi minimum tensile class, S marks a solid wire, and 6 is the deoxidizer level, higher than the 3 in ER70S-3. The governing document is the AWS A5.18 specification, published by the American Welding Society. Hobart lists this wire under its HB-28 trade name.
Can this wire weld stainless steel or aluminum?
No. This is a carbon steel wire for mild steel work. Stainless jobs need ER308L-class wire with a high-argon or tri-mix gas, and aluminum needs ER4043 or ER5356 with 100% argon.
Conclusion
The Hobart ER70S-6 .035 in. 10 lb spool is the budget pick I recommend without hedging. You get brand-name consistency, published classification data, and a deoxidizer package that forgives ordinary dirty steel, all at a per-pound price that undercuts the premium names. Run it on 75/25, keep it dry after opening, and it lays flat, clean beads all day on fabrication, farm, and auto work. Mind the packaging in shipping and storage and there is nothing left to complain about. To see how it stacked up against the seven other wires we tested, read our best MIG welding wire guide.